
Manufacturers are under constant pressure to produce more.
More customer orders. More customized products. Shorter lead times. Higher expectations for on-time delivery.
But increasing production isn’t always as simple as hiring more employees, purchasing additional equipment, or expanding factory space.
In many manufacturing environments, unused capacity already exists. The challenge is identifying where production is being constrained and finding ways to use existing resources more effectively.
That’s where manufacturing capacity planning becomes essential.
For make-to-order manufacturers producing cabinets, windows, doors, furniture, millwork, metal components, and other configurable products, effective capacity planning can help increase throughput, improve scheduling, reduce bottlenecks, and support growth without immediately increasing overhead.
As manufacturers begin planning for 2027, understanding how to get more from existing operations is becoming an important competitive advantage.
What Is Manufacturing Capacity Planning?
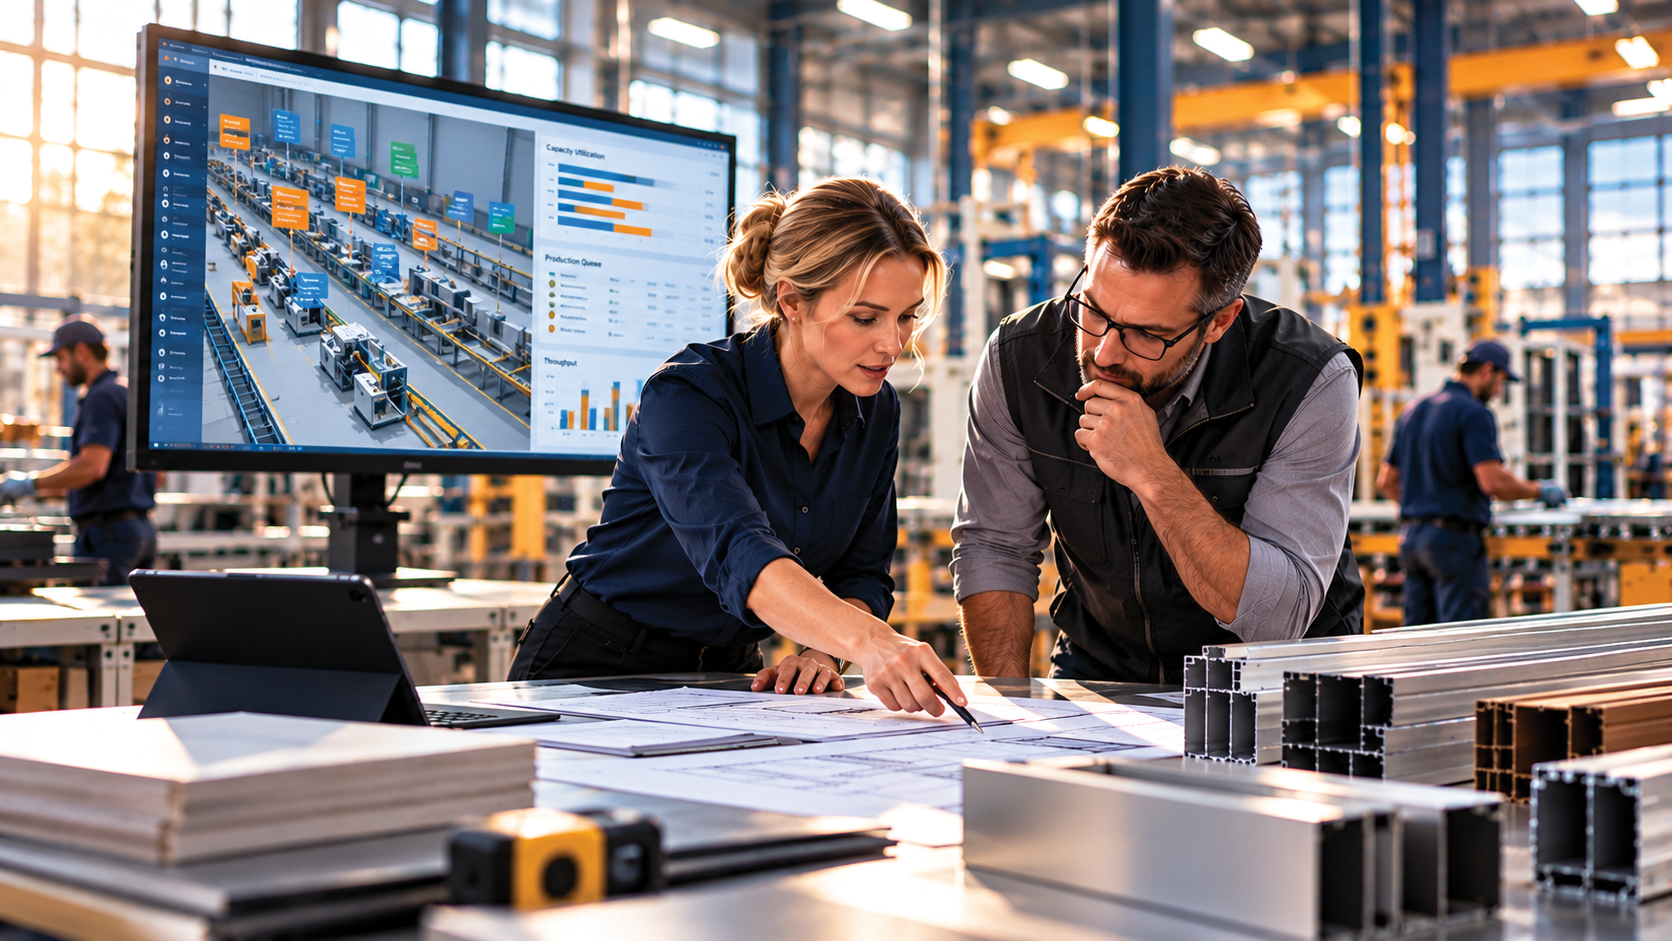
Manufacturing capacity planning is the process of determining whether a manufacturer has sufficient resources to meet current and anticipated production demand.
Those resources include:
- Available machinery and equipment
- Labor and employee skills
- Work center availability
- Production hours and shifts
- Material availability
- Manufacturing processes
- Customer delivery requirements
Effective capacity planning helps manufacturers balance demand against available resources while identifying potential constraints before they disrupt production.
Two common approaches include:
Rough-Cut Capacity Planning (RCCP): Evaluates whether overall production capacity can support the master production schedule.
Detailed Capacity Requirements Planning (CRP): Examines resource requirements at individual work centers and operations to identify more specific capacity constraints.
Together, these approaches help manufacturers understand both the bigger production picture and the operational details affecting throughput.
1. Identify the Real Production Bottlenecks
One of the biggest mistakes manufacturers make is assuming that every work center needs to operate faster.
In reality, production throughput is often limited by a small number of constraints.
For example, a cabinet manufacturer might have sufficient cutting capacity but experience delays in finishing or assembly.
Increasing cutting output won’t necessarily improve overall throughput if unfinished products simply accumulate before the next operation.
Manufacturers should evaluate:
- Which work centers consistently have backlogs
- Where work-in-progress inventory accumulates
- Which operations experience frequent delays
- Whether equipment downtime affects downstream production
- How labor availability influences capacity
By identifying the actual constraint, manufacturers can focus improvement efforts where they will have the greatest impact.
The goal isn’t to make every machine busier. It’s to make the entire operation more productive.
2. Move Beyond Static Production Schedules
Traditional production schedules often rely on spreadsheets or manually maintained planning boards.
These tools can work in smaller environments, but they become difficult to manage as manufacturing complexity increases.
Customer priorities change.
Materials arrive late.
Equipment requires maintenance.
Employees become unavailable.
Urgent orders enter the schedule.
A static schedule can quickly become outdated.
Integrated manufacturing ERP software helps planners work with more current information about available capacity, material requirements, production priorities, and customer commitments.
For manufacturers managing configurable products, that flexibility is particularly important because different orders may require different production resources.
3. Use Finite Capacity Scheduling
One of the most valuable approaches to improving capacity planning is finite capacity scheduling.
Traditional infinite capacity planning assumes production resources can accommodate scheduled demand without fully accounting for resource limitations.
Finite capacity scheduling considers actual constraints.
These may include:
- Machine availability
- Work center capacity
- Labor resources
- Setup and run times
- Production sequences
- Material availability
For example, if a work center has 40 available production hours but scheduled work requires 55 hours, the manufacturer has a 15-hour capacity gap.
A finite capacity approach makes that constraint visible.
Planners can then evaluate options such as adjusting priorities, shifting work, reducing setup time, adding temporary capacity, or revising delivery commitments.
This creates more realistic production schedules and helps manufacturers avoid making commitments that available resources cannot support.
4. Reduce Setup and Changeover Time
Manufacturers producing configurable products often experience frequent production changeovers.
A window manufacturer may switch between frame types, dimensions, colors, or hardware requirements.
A cabinet manufacturer may move between materials, finishes, and product configurations.
A metal manufacturer may need to change tooling, profiles, or fabrication requirements.
Every changeover can consume valuable production capacity.
Manufacturers can improve throughput by:
- Grouping similar jobs
- Optimizing production sequences
- Standardizing setup procedures
- Preparing materials in advance
- Improving coordination between work centers
- Identifying unnecessary equipment adjustments
Even modest reductions in setup time can create additional productive hours.
For example, saving 15 minutes across eight daily changeovers creates two additional hours of available capacity each day.
Over a five-day workweek, that’s 10 hours of potential capacity recovered without purchasing another machine.
5. Connect Material Planning With Production Capacity
A machine may be available.
Employees may be ready.
The production schedule may be open.
But if the required material hasn’t arrived, the capacity cannot be used effectively.
This is why capacity planning and material requirements planning must work together.
Manufacturers need visibility into:
- Available inventory
- Allocated materials
- Open purchase orders
- Supplier lead times
- Bills of materials
- Production requirements
- Planned start dates
Integrated ERP helps connect these activities so planners can evaluate production requirements alongside material availability.
This reduces the risk of scheduling work that cannot actually begin.
For make-to-order manufacturers, where material requirements can vary significantly between orders, this connection is especially valuable.
6. Improve Labor Utilization Without Simply Adding Headcount
Labor remains a critical component of manufacturing capacity.
However, adding employees isn’t always the fastest or most cost-effective way to increase output.
Manufacturers should first evaluate how existing labor resources are being used.
Consider questions such as:
- Are employees waiting for materials or instructions?
- Do workers spend time searching for updated drawings?
- Are skilled employees performing repetitive administrative tasks?
- Are production assignments balanced across available resources?
- Could better scheduling reduce overtime?
- Are certain operations dependent on only one experienced employee?
Improving access to information, standardizing workflows, and reducing unnecessary manual tasks can help employees spend more time on productive activities.
The objective isn’t simply to increase labor hours.
It’s to increase the value created during those hours.
7. Monitor Capacity and Throughput With Operational KPIs
Manufacturers cannot improve capacity planning without understanding current performance.
Useful manufacturing capacity KPIs include:
| KPI | What it measures |
|---|---|
| Capacity utilization | Percentage of available production capacity being used |
| Manufacturing throughput | Units or orders completed during a defined period |
| Work center utilization | How effectively individual production resources are used |
| Schedule adherence | How closely actual production follows the planned schedule |
| Setup and changeover time | Time consumed preparing equipment for different jobs |
| Work-in-progress (WIP) | Inventory currently moving through production |
| On-time delivery | Percentage of orders delivered by their committed dates |
These metrics help manufacturers identify constraints, evaluate scheduling decisions, and determine whether operational improvements are producing results.
However, utilization should not be viewed in isolation.
A work center operating at 100% utilization isn’t necessarily improving the business if it creates excess inventory or produces items that downstream operations cannot process.
The most useful metrics are those that reflect the performance of the entire manufacturing operation.
Capacity Planning vs. Production Scheduling: What’s the Difference?
Although closely related, capacity planning and production scheduling serve different purposes.
Capacity planning determines whether sufficient resources exist to meet demand.
Production scheduling determines when specific work should be performed and which resources should complete it.
For example, capacity planning may identify that a finishing department needs 120 labor hours next week but has only 100 available.
Production scheduling then determines how individual jobs should be sequenced or adjusted within those constraints.
When both functions are connected through ERP, manufacturers can create more realistic plans and respond more effectively when conditions change.
How to Calculate Manufacturing Capacity Utilization
A basic capacity utilization calculation is:
Capacity Utilization (%) = (Actual Output ÷ Maximum Practical Output) × 100
For example, assume a manufacturing work center has a practical weekly capacity of 500 units.
If it produces 400 units:
(400 ÷ 500) × 100 = 80% capacity utilization
This indicates that the work center is operating at 80% of its defined practical capacity.
However, manufacturers should consider additional factors, including product mix, setup requirements, labor availability, equipment downtime, and quality performance.
For make-to-order operations, capacity measured in standard production hours may be more meaningful than units alone.
Why Capacity Planning Is More Challenging for Make-to-Order Manufacturers
Standardized production environments often have predictable routings and relatively consistent processing times.
Make-to-order manufacturers operate differently.
Every order may include variations in:
- Product dimensions
- Materials
- Components
- Engineering requirements
- Production routing
- Setup time
- Labor requirements
- Customer delivery dates
These variables make it difficult to rely on simple averages when planning capacity.
A manufacturer may have enough total production hours available but lack sufficient capacity at one specific work center.
Effective capacity planning therefore requires detailed information about both product requirements and manufacturing resources.
How Frontier ERP Supports Manufacturing Capacity Planning
Frontier ERP is designed for complex make-to-order manufacturing environments where production planning must account for changing customer requirements, product configurations, and resource constraints.
Frontier supports both rough-cut and detailed capacity planning, helping manufacturers evaluate capacity limitations across sales order processing, material planning, and production scheduling.
Its manufacturing management capabilities include:
- Master Production Scheduling (MPS)
- Material Requirements Planning (MRP)
- Capacity Requirements Planning (CRP)
- Production scheduling
- Work center management
- Inventory and purchasing integration
- Manufacturing reporting
Frontier’s production scheduling capabilities also support finite constraint-based work center scheduling, forward and backward scheduling, and production grouping based on user-defined criteria.
These capabilities help manufacturers coordinate production requirements while improving visibility into available resources.
For organizations managing complex products, integrating capacity planning with product configuration, inventory, and manufacturing data provides a stronger foundation for operational decision-making.
Planning for 2027: Can Your Existing Factory Support More Growth?
As manufacturers begin developing their 2027 operational plans, capacity should be part of the conversation.
Before approving another equipment purchase or facility expansion, manufacturers should ask:
Where is our current capacity being lost?
The answer may involve:
- Excessive changeover time
- Unbalanced production schedules
- Material shortages
- Equipment downtime
- Manual information transfers
- Inaccurate planning assumptions
- Poor visibility into work center constraints
Some capacity challenges will require additional investment.
But others may be addressed through better planning, scheduling, process improvements, and integrated technology.
Understanding the difference can help manufacturers make smarter capital investment decisions.
One Platform. Smarter Manufacturing. Stronger Business.
For manufacturers, sustainable growth requires more than increasing production volume.
It requires coordinating people, materials, equipment, customer orders, and financial resources effectively.
That’s the direction behind Frontier ERP and the evolution toward Frontier 5.0.
By connecting critical manufacturing processes through a common operational foundation, manufacturers can improve visibility, reduce unnecessary complexity, and make more informed decisions about capacity.
The goal isn’t simply to produce more. It’s to produce more efficiently, predictably, and profitably.
Conclusion
Increasing manufacturing throughput doesn’t always require a larger factory.
For many manufacturers, the first opportunity lies in making better use of existing resources.
By identifying bottlenecks, implementing finite capacity scheduling, reducing changeover time, connecting material planning, improving labor utilization, and monitoring operational KPIs, manufacturers can uncover opportunities to increase output while controlling costs.
For make-to-order manufacturers, integrated ERP technology helps bring these activities together.
As businesses prepare for 2027, better manufacturing capacity planning can provide a practical path toward greater productivity, stronger delivery performance, and sustainable growth.
Frequently Asked Questions
What is manufacturing capacity planning?
Manufacturing capacity planning is the process of evaluating available equipment, labor, materials, and production resources to determine whether a manufacturer can meet current and future demand.
How can manufacturers increase throughput without expanding their facilities?
Manufacturers can increase throughput by eliminating bottlenecks, reducing setup time, improving production scheduling, minimizing downtime, and using existing resources more efficiently.
What is finite capacity scheduling?
Finite capacity scheduling is a production planning approach that considers actual resource constraints, such as machine availability, labor, work center capacity, and setup times, when creating schedules.
How does ERP improve manufacturing capacity planning?
ERP connects production scheduling, inventory, purchasing, material requirements, customer orders, and resource information, helping manufacturers create more realistic production plans.
What is the difference between capacity planning and production scheduling?
Capacity planning determines whether enough resources are available to meet demand. Production scheduling determines when specific jobs should be completed using those resources.
Why is capacity planning important for make-to-order manufacturers?
Make-to-order manufacturers manage products with varying materials, configurations, processing times, and production requirements. Capacity planning helps ensure these orders can be manufactured using available resources.